Premium efficiency three-phase, brushless, and high-voltage induction motors tailored for industrial OEM/ODM supply across Australian sector operations.

A Technical Whitepaper on OEM/ODM Customization, Thermal Endurance, and Efficiency Standards
Australia’s industrial sector operates under some of the world’s most demanding environmental and operational parameters. From the dust-laden, high-ambient thermal conditions of the Pilbara mining region in Western Australia to the highly corrosive coastal marine terminals along the eastern seaboard, heavy rotating equipment must maintain uninterrupted duty cycles. High Voltage (HV) induction motors—operating typically at 3.3kV, 6.6kV, and 11kV grid connections—serve as the prime movers for critical infrastructure including slurry pumps, mine ventilation fans, overland conveyors, gas compressors, and seawater desalination systems.
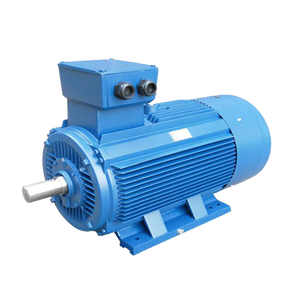
As a global leader in OEM and ODM electric motor manufacturing with over 50 years of specialized application expertise, our engineering teams design custom high-voltage squirrel-cage and wound-rotor induction motors specifically configured for Australian operational frameworks. Through advanced electromagnetic modeling, high-grade Vacuum Pressure Impregnation (VPI) insulation systems, and dynamic mechanical optimization, we deliver fit-for-purpose motor drives that yield significant total cost of ownership (TCO) reductions and eliminate catastrophic unplanned downtime.
Tailored engineering configurations designed to solve industry-specific challenges across the continent.
Mining operations require robust heavy-duty drives capable of withstanding ambient temperatures exceeding 50°C and severe fine particulate dust (iron ore, bauxite, coal). Our custom ODM high-voltage induction motors feature heavy cast-iron or fabricated steel frames, IC611 air-to-air heat exchangers, IP66 dust-tight enclosures, and reinforced copper bar rotors. They provide exceptional pull-out torque ratios to handle shock loading in heavy primary jaw crushers and SAG mills.
Australia’s severe water scarcity accentuates the importance of large-scale reverse osmosis desalination plants and cross-regional water transfer networks. We engineer high-efficiency 6.6kV and 11kV pump-drive motors equipped with duplex stainless steel shafts, C5-M marine-grade multi-layer epoxy coatings, and active anti-condensation heating systems. These features protect internal stators against saline humidity while achieving IE4/IE5 efficiency thresholds to lower continuous pumping electricity expenses.
Continuous industrial processing facilities require motors capable of long continuous duty (S1) under variable speed operation via Variable Frequency Drives (VFDs). Our OEM custom solutions incorporate insulated non-drive-end (NDE) bearings or grounding rings to prevent micro-sparking bearing erosion caused by Common Mode Voltage (CMV). Stator windings are treated with inverter-duty crown phase insulation to resist high voltage spikes (dv/dt).
Offshore gas extraction platforms and bulk material handling sea terminals require explosion-proof (Ex d / Ex e / Ex nA) motor designs certified to global standards. Our heavy-duty high voltage motors are built to withstand severe axial and radial forces experienced on marine thrusters, cargo pumps, and terminal winches, backed by comprehensive marine classification certificates (ABS, DNV, BV, LR).
Understanding the transition toward net-zero industrial targets, grid stability requirements, and digital monitoring in Australia.
| Regulatory / Industry Driver | Technical Impact on HV Motor Design | Our Engineering & OEM Custom Solution |
|---|---|---|
| AS/NZS 60034 & GEMS/MEPS Compliance | Mandatory efficiency thresholds to reduce industrial carbon footprints and grid stress across national energy networks (NEM). | Precision electromagnetic slot layout, low-loss silicon steel laminations, and premium copper volume maximizing efficiency up to IE4/IE5 levels. |
| Extreme Ambient Operating Envelope (Up to 55°C) | Standard off-the-shelf motors suffer severe thermal derating, leading to premature insulation breakdown and bearing failure. | Class H VPI insulation, oversized IC611/IC81W heat exchangers, synthetic high-temp greases, and custom thermal calculation models. |
| Remote Site IoT Telemetry Integration | Mining hubs located thousands of kilometers from capital cities require real-time condition monitoring to prevent unexpected failures. | Factory integration of PT100 RTD sensors in windings/bearings, SPM vibration monitoring nipples, and smart IoT telemetry junction boxes. |
| Integration with Renewable Microgrids | Industrial sites relying on localized solar/wind microgrids experience voltage fluctuations and transient harmonics. | Enhanced dielectric strength insulation withstand capabilities, reinforced mechanical shaft torque limits, and customizable terminal boxes. |
From initial electromagnetic design to final site commissioning support, we deliver tailored rotation solutions.
We modify mechanical mounting dimensions to align perfectly with legacy installations, replacing aging motor populations without costly civil or piping modifications. Shaft material selections include 4140 high-tensile steel, 316 stainless, or Duplex steels with custom keyway profiles, foot/flange arrangements (B3, B5, V1, B35), and heavy-duty roller bearings for high radial loads.
Winding designs tailored for specific starting current limits (e.g., 600% or 450% I_n) required by remote regional power grids with limited fault capacity. Custom pole-changing windings, multi-voltage tap connections (3.3kV / 6.6kV dual voltage capability), and custom torque speed curves optimized for high-inertia loads like large blowers and crushers.
Depending on ambient environmental factors, we supply cooling topologies across IC411 (Totally Enclosed Fan Cooled), IC611 (Totally Enclosed Air-to-Air Cooled), IC81W (Totally Enclosed Water-to-Air Cooled), and IC01 (Open Drip-Proof). Enclosures are rated from IP55 up to IP66 and IP67 for submerged or washdown duty environments.
Essential guidance on specifications, certification, delivery, and support for Australian industrial buyers.
Combining 50+ years of industrial legacy, global logistics prowess, and uncompromised quality assurance.
Decades of field experience in heavy industry ensure every motor design is backed by validated electromagnetic calculations and proven metallurgical standards. We eliminate premature field failures through proactive engineering oversight.
Our high-voltage test center supports full automated load testing up to 13.8kV grid simulator capabilities. Stator core loss testing, dynamic balancing to G1.0 standards, and full partial discharge verification ensure long-term dielectric performance.
Australian clients benefit from a single point of technical contact throughout the purchasing, engineering review, manufacturing, and delivery cycle. We manage documentation, GA drawings, 3D CAD step files, and test certificates with total transparency.
Connect directly with our senior electrical application engineers. We provide comprehensive technical quotes, custom 2D/3D CAD dimensional models, and AS/NZS compliance reviews for your OEM or MRO requirements.
