Engineering Architecture of Heavy-Duty Compressor Motors
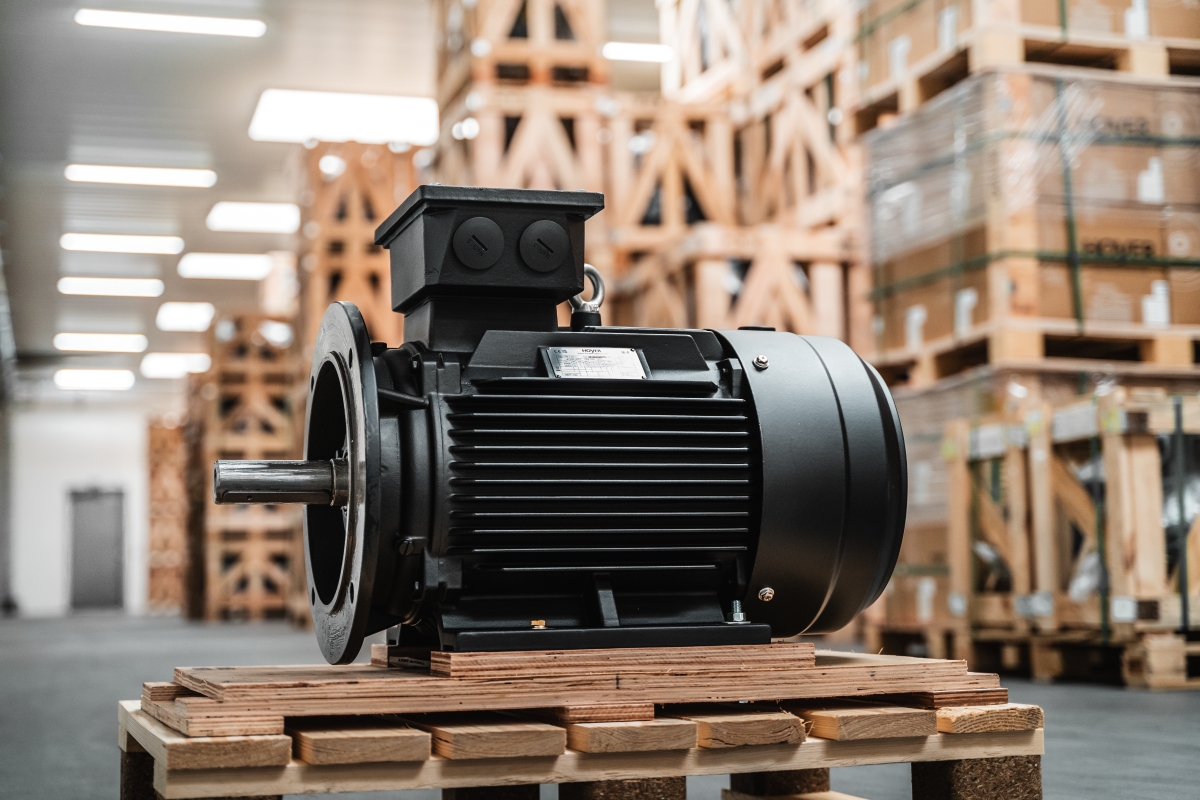
Industrial compressed air systems account for approximately 10% of all global electrical energy consumed in manufacturing plants. As the core mechanical driver of positive displacement screw compressors and reciprocating piston pumps, heavy-duty electric motors operate under severe thermodynamic, mechanical, and electrical stresses. Selecting a top-tier motor manufacturer requires deep scrutiny of electromagnetic design, insulation dynamics, thermal dissapation, and bearing fatigue life.
Core Rule of Information Gain: Standard off-the-shelf industrial motors frequently fail in air compressor duty due to rapid start-stop thermal spikes, unloader valve pressure transients, and high radial forces transmitted through direct couplings or drive belts. OEM-grade compressor motors must be engineered specifically for S1 continuous duty with elevated Service Factors (SF 1.15 to 1.25).
1. Inverter-Duty Insulation & Voltage Spike Mitigation (dV/dt)
With the widespread adoption of Variable Frequency Drives (VSD / VFD) to optimize compressor energy performance, electric motor stator windings are exposed to extreme high-frequency pulse-width modulation (PWM) voltage waveforms. Standard copper magnet wire insulation suffers from micro-partial discharge (corona effect), leading to rapid dielectric breakdown and premature inter-turn short circuits.
Our heavy-duty compressor motors utilize Class H insulation systems rated for 180°C operation, impregnated via full Vacuum Pressure Impregnation (VPI) with solventless epoxy resin. This process guarantees void-free winding encapsulation, providing exceptional resistance to dV/dt voltage spikes exceeding 1600V/μs, high humidity, oil mist contamination, and thermal expansion fatigue.
2. Bearing Dynamic Load Ratings & L10h Life Optimization
Over 55% of premature industrial motor failures stem from mechanical bearing degradation caused by heavy radial belt loads, axial screw rotor thrust, and shaft current erosion (EDM fluting). Top-trusted motor factories integrate specific mechanical safeguards:
Heavy-Duty SKF/NSK Bearings
Sized for calculated L10h bearing life exceeding 100,000 operating hours under continuous rated loads, using premium synthetic high-temperature polyurea grease.
Shaft Grounding & Insulated Bearings
To eliminate electrical discharge machining (EDM) caused by VFD common-mode voltages, non-drive end (NDE) ceramic-coated insulated bearings and micro-fiber grounding rings are fitted as standard.
Regreasing System & SPM Ports
Equipped with external regreasing nipples and SPM vibration monitoring ports on both drive-end (DE) and non-drive-end (NDE) shields for real-time predictive maintenance.
Compressor Motor Engineering Specification Matrix
| Technical Parameter | Standard Industrial Motor | Heavy-Duty OEM Compressor Motor | Impact on Compressor Operational Reliability |
|---|---|---|---|
| Efficiency Class | IE2 or IE3 (Standard) | IE4 Super Premium / IE5 SynRM | Reduces total electrical utility cost by 3% to 8% per year. |
| Service Factor (SF) | 1.00 – 1.10 | 1.15 – 1.25 (Continuous) | Prevents thermal tripping during high pressure unloader spikes. |
| Insulation & Temp Rise | Class F (80K Rise) | Class H Insulation with Class B Rise | Extends winding insulation operating lifespan by over 200%. |
| Ingress Protection | IP54 / IP55 | IP55 / IP66 Cast Iron Frame | Protects against particulate dust, aggressive humidity, and oil vapor. |
| VFD Protection | Optional / Standard Wire | VPI + Insulated NDE Bearings + Grounding | Eliminates bearing EDM pitting and winding corona degradation. |