Precision-engineered, CE-compliant 3-phase, BLDC, and asynchronous motors designed for rigorous duty cycles, robotics, heavy industrial pumping, and global OEM machinery.
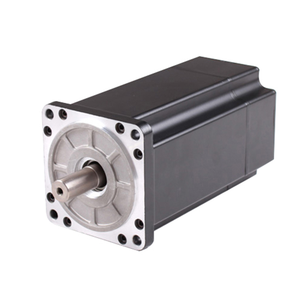
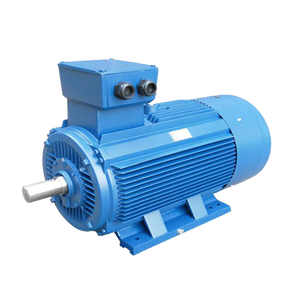
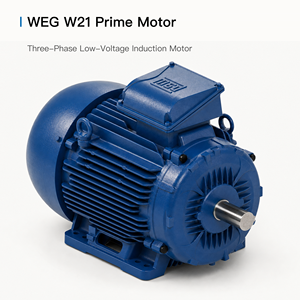
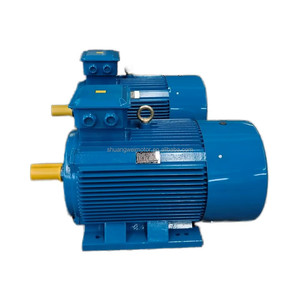
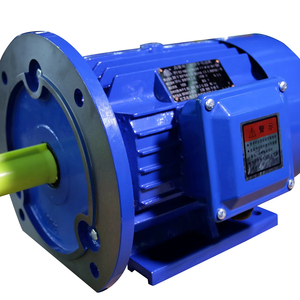
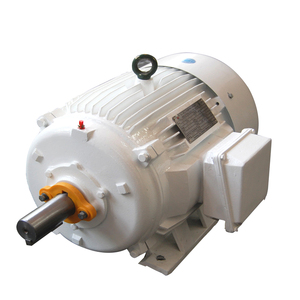
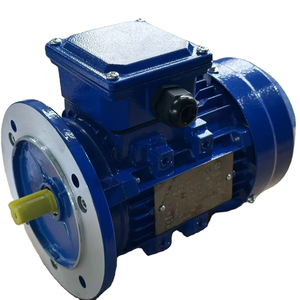
In modern industrial manufacturing, electrical safety, mechanical reliability, and electromagnetic compatibility are non-negotiable prerequisites. A certified CE Certified Industrial Gear Motor serves as the mechanical heart for automated conveyors, heavy chemical agitators, marine winches, and municipal water purification pumps. Achieving genuine CE marking requires strict adherence to mandatory European Union Directives, including the Low Voltage Directive (LVD) 2014/35/EU, Electromagnetic Compatibility (EMC) Directive 2014/30/EU, and the Machinery Directive 2006/42/EC.
As a premier industrial motor manufacturer, our factory operations integrate stringent quality assurance systems certified under ISO 9001, ISO 14001, and ISO 45001. Every gear motor assembly undergoing factory acceptance testing (FAT) is subjected to rigorous insulation resistance testing, high-voltage withstand checks, dynamic rotor balancing, and acoustic noise level measurements according to IEC 60034-1 standards.
Under recent European eco-design legislation, electric motors ranging from 0.75kW to 1000kW must comply with minimum IE3 (Premium Efficiency) standards, with 75kW to 200kW requirements mandating IE4 (Super Premium Efficiency) compliance. Our gear motors incorporate low-loss silicon steel laminations, 100% oxygen-free electrolytic copper windings, and optimized slot filling to minimize stator copper loss ($P_{cu1}$) and rotor aluminum/copper bar loss ($P_{cu2}$).
Verified dielectric strength testing at 2x rated voltage + 1000V for 60 seconds. Thermal Class H (180°C) insulation systems operating well within Class B temperature rise bounds (80K limit) for prolonged insulation lifespan.
Integrated shaft grounding rings and shielded terminal box designs block common-mode currents and high-frequency PWM harmonics generated by Variable Frequency Drives (VFDs), preventing bearing fluting and capacitive discharge damage.
For hazardous operating zones, our certified flameproof Ex d, Ex db, and increased-safety Ex eb gear motor lines block thermal transfer and internal spark ignition, conforming to EN 60079-0/1 standards.
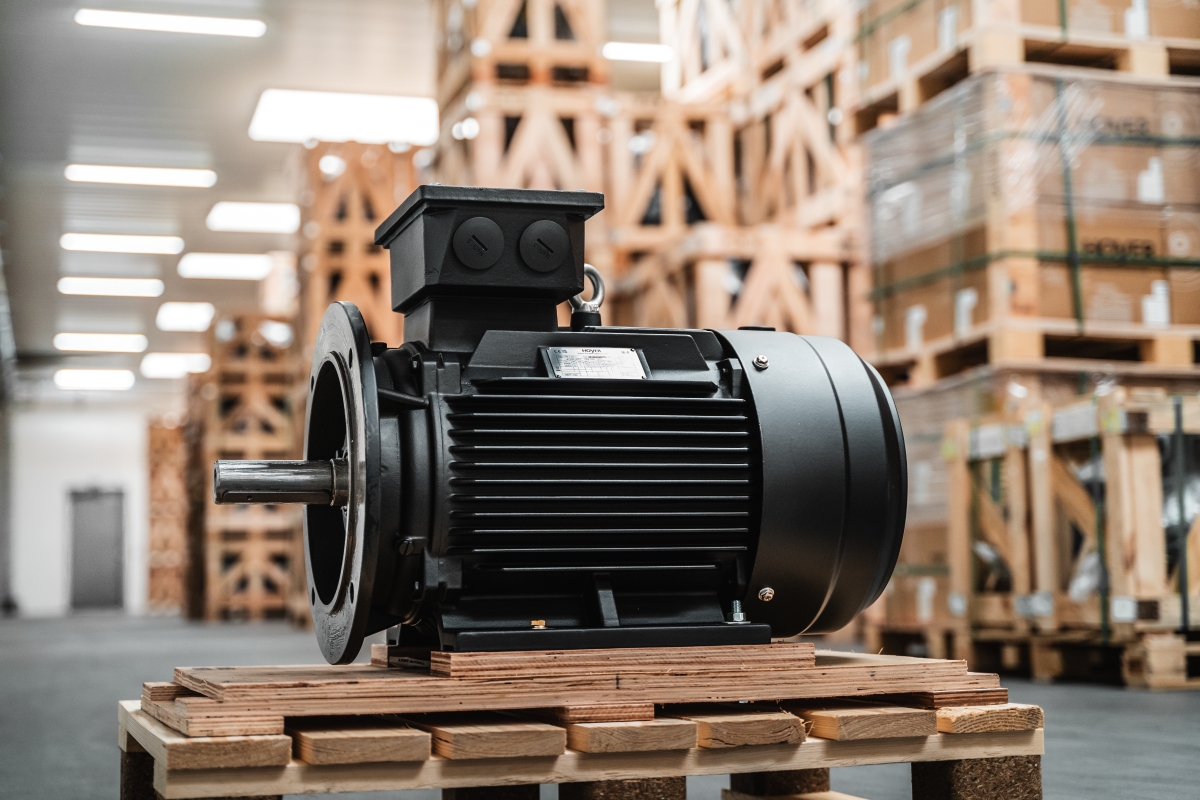
Combining high-efficiency electric motors with planetary, helical, bevel, or worm gear reducers requires micro-micron tolerance alignment. Our CNC tooth-grinding facilities execute DIN 3962 Class 5 gear grinding to achieve high gear mesh contact ratios, reducing backlash to < 3 arcmin for precision servo applications and lowering acoustic noise below 62 dB(A).
Whether you require foot-mounted (B3), flange-mounted (B5/B14), or face-and-foot configurations (B35), our modular casing options in high-tensile gray cast iron (GG20/GG25) or die-cast aluminum alloys deliver structural rigidity against dynamic torsional shocks.
Selecting the optimal gear motor configuration requires matching electric motor electrical parameters with gearbox mechanical output ratings. The table below outlines key technical thresholds across our core CE-certified series:
| Motor Series | Efficiency Rating | Power Range (kW) | Enclosure Class | Gearhead Pairing Options | Primary Industrial Use Case |
|---|---|---|---|---|---|
| IE4 Super Premium | IE4 / NEMA Super Premium | 0.75kW – 375kW | IP55 / IP65 / IP66 | Helical Inline, Bevel Helical | Continuous Process Pumps, Heavy Compressors, Extruders |
| IE3 Premium Efficiency | IE3 / NEMA Premium | 0.12kW – 1000kW | IP55 / IP56 | Helical-Worm, Parallel Shaft | Conveying Systems, Agitators, Industrial Fans |
| NEMA 42 High-Speed BLDC | > 90% Brushless DC | 1.0kW – 3.0kW | IP65 Marine/Robotic | Precision Planetary Reducers | Autonomous Mobile Robots (AMRs), Automated Guided Vehicles |
| Flameproof Ex d / Ex db | IE2 / IE3 Certified | 0.37kW – 315kW | IP66 Hazardous Zone | Heavy-Duty Steel Helical | Oil & Gas Refineries, Chemical Processing, Mining Conveyors |
| Y3 / High Power Cast Iron | IE2 / IE3 Heavy Power | 160kW – 800kW | IP55 Cast Iron | Industrial Heavy Bevel Gearbox | Mining Crushers, Large Centrifugal Blowers, Marine Thrusters |
As global supply chains navigate energy transition imperatives, raw material volatility, and Industry 4.0 automation demands, B2B procurement managers and OEM design directors must anticipate shifts in drivetrain specification. Key technological vectors reshaping the industrial motor landscape include:
While induction motors remain the industry workhorse, the transition toward IE5 Ultra-Premium Efficiency is accelerating. Synchronous Reluctance Motors eliminate rotor copper loss by operating without rotor currents or rare-earth permanent magnets. When coupled with high-efficiency helical gearboxes, SynRM drivetrains reduce total energy dissipation by up to 40% compared to legacy IE2 systems, significantly lowering lifecycle Operating Expenditure (OPEX).
Modern industrial buyers are moving away from reactive or time-based maintenance schedules. Factory-fitted wireless IoT vibration sensors, embedded PT100/PT1000 stator thermistors, and acoustic emission transducers stream real-time operational data directly to SCADA or cloud-based analytics platforms. Early detection of bearing race micro-spalling, gear tooth pitting, or voltage imbalance prevents catastrophic machine failures and unplanned factory downtime.
The standard off-the-shelf model is increasingly unable to satisfy niche OEM demands. Forward-thinking manufacturers maintain large buffer inventories of modular components—such as specialized extended shafts, dual-ended shafts, customized mounting flanges, low-temperature synthetic lubricants, and heavy-duty C4/C5M marine anti-corrosion paint treatments. Maintaining over 70,000 baseline motors in strategic regional warehouses enables rapid engineering conversion and rapid dispatch within 24 to 48 hours.
With over 50 years of application-driven engineering heritage, our facility operates as a consolidated solution provider for power and motion systems. Built on the combined expertise of specialized motor manufacturing and extensive aftermarket MRO services, we provide end-to-end support for mission-critical marine and land-based industrial operations.
Our centralized distribution hubs in Northern Europe and APAC (Ningbo) maintain massive physical inventories of standard IE2, IE3, IE4, and brake motors, insulating OEM procurement teams from supply chain shocks.
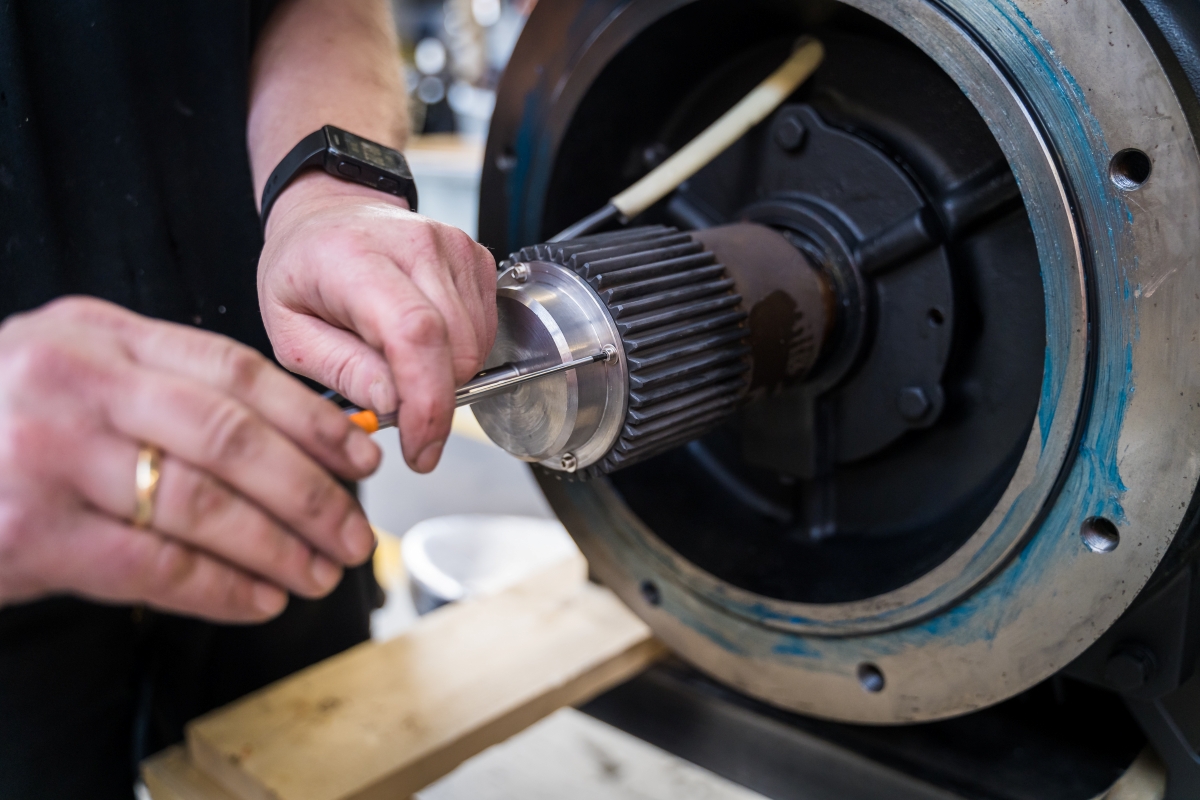
Equipped with computerized dynamometer test benches, climatic environmental chambers, and precision balancing rigs, our engineering team executes custom shaft machining, encoder retrofits, and forced-cooling fan installations.
Global field service engineers and rapid spare parts logistics guarantee round-the-clock technical emergency support, minimizing downtime risk for offshore vessels, power stations, and continuous process lines.
Below are expert answers to common technical queries raised by electrical engineers, machinery designers, and global sourcing managers when specifying CE-certified gear motors:
Partner with an established CE-certified gear motor manufacturer. Our application engineers are ready to assist with CAD models, custom electrical design, thermal calculations, and competitive OEM volume pricing.
